Hey there, welcome to my corner of the web – if you stumbled here because you just unboxed your first resin 3D printer or you’re actually the manager of a small design shop thinking about ditching fdm for something way more detailed, you’re in the right place. I’ve been supplying resin printers for almost a decade, and let me tell you, the biggest mistake new users make is overcomplicating the setup, right? Like, I get it – resin printers look fancy, all those tiny parts and that smelly liquid that looks like paint thinner your cousin brought to Thanksgiving. But if you take it step by step, it’s way less terrifying than it sounds. No, you won’t accidentally turn your room into a lab (I promise), and no, you don’t need an engineering degree to pull this off. Let’s break this down like we’re chatting over coffee, not reading a instruction manual that’s 50 pages long. Resin 3D Printer
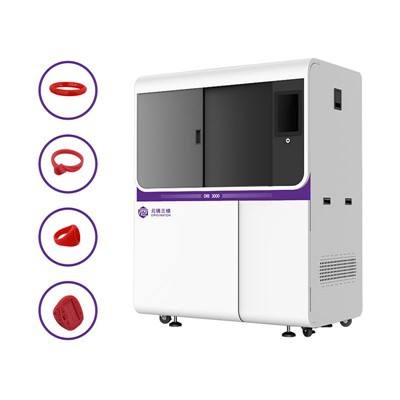
First things first, let’s talk about the stuff you’ll need right out of the box. When I ship a printer to someone, the last thing I want is them digging through their closet for random supplies at 10 PM on a Saturday, panicking because they can’t find a key part. So let’s keep this simple: you’re gonna need resin, obviously. But not just any resin. Wait, no, hold on – don’t buy the cheapest bulk resin on Amazon. I know it’s tempting, but that’s how you get lumpy prints that cure unevenly, or resin that gums up your tank in a week. Stick to the resin I recommend for your printer model – I’m not just saying that because I sell it, I’ve tested this stuff for years. Different printers have different UV light intensities, and using the wrong resin means your prints either won’t cure at all or will turn brittle like a old potato chip. Also, pick a resin color that works for your first test print – white or gray is perfect, no fancy tints to mess with your eyes when you’re checking for cure.
Next, you need something to hold the resin. Wait, the printer usually comes with a resin tank, right? But you’ll need a separate container for cleaning prints later – a old plastic tub or even a glass jar works, as long as it’s not going to be used for food ever again. And the most important thing for beginners: isopropyl alcohol, or IPA. Not the stuff you use to clean your phone, the 91% or higher kind. 70% is too weak, it’ll leave residue on your prints that makes them feel sticky forever. A 1 liter bottle of 91% IPA will last you for like 20 prints, so don’t go buying a gallon right away – start small, test the waters. Oh, and some paper towels or lint-free cloths. Lint is the enemy here. If you use a regular paper towel, you’ll leave little fibers all over your print that you have to pick off later. Lint-free cloths are worth the extra couple bucks.
Now, let’s get to the actual setup. First, unboxing. Don’t just tear the box open like you’re on TikTok unboxing spree. Take your time, pull each part out carefully – the FEP film on the resin tank is super delicate, one tiny scratch and you’re replacing that whole tank, which is an extra $50 you don’t need to spend. Lay everything out on a flat, stable surface – no wobbly desks, that’s a disaster waiting to happen. If your desk shakes when you type, move the printer to a table that’s solid. Once everything’s out, the first step is assembling the frame. Most modern resin printers (the ones I supply, anyway) are tool-free or only need a tiny screwdriver, so this takes like 10 minutes. No need to call a friend over for this part, I promise.
Next, leveling the build plate. This is the make-or-break step, and I see so many new users mess this up. If the build plate isn’t level, your first print will have one side not sticking, or it’ll be way too close to the FEP film and stick like glue, ruining both the print and the tank. How to level it? Most printers have a leveling function where you loosen the build plate screws, then use the little paper test method. Slip a piece of printer paper between the build plate and the FEP film, then tighten each screw until the paper pulls with a little resistance. Do this for all four corners, and maybe the middle too if your printer has that. Pro tip: don’t overtighten, that warps the build plate. I’ve had customers tell me they ruined three FEP films in a week because they over-tightened the build plate – don’t be that person.
Once the build plate is level, it’s time to load the resin. Here’s where a lot of people make that “oops” face. First, make sure the tank is clean – wipe the inside of the bottom of the tank with a little IPA and a lint-free cloth, no leftover resin gunk. Then, pour the resin slowly into the tank, don’t just dump it. Fill it up to the line on the tank – every tank has a little max fill line, don’t go over that. If you pour too much, resin will leak out when the build plate moves, and that’s a mess. And close the tank lid, obviously – you don’t want resin spilling if you bump the table. Quick note: keep resin away from kids and pets, it’s toxic if ingested, and if it gets on your skin, wash it off right away with soap and water. No big deal, just be careful.
Now, you need a 3D model to print. Don’t go downloading that super detailed 10-inch dragon model right away. Start small. Go to Thingiverse or MyMiniFactory, they have tons of free, pre-supported models for beginners. Pre-supported means the model already has those little stick-like supports that hold it up during printing, so you don’t have to design supports yourself – that’s another thing that scares new users. Pick something tiny, like a keychain or a small figurine, that takes 15 or 20 minutes to print. Why short? Because your first print will almost definitely not be perfect. If you’re waiting 2 hours for a print to fail, that’s a huge letdown. Short prints let you troubleshoot fast without wasting a bunch of resin or time.
Now, slicing. Slicing is just the process of taking your 3D model and turning it into tiny layers the printer can read, right? Most resin printers come with their own free slicer software, which is perfect for beginners – don’t go using a random slicer you found online unless you know what you’re doing. Load your model into the slicer, make sure it’s the right size, rotate it if you need to, then add supports if it’s not pre-supported. Wait, most beginners should just stick to pre-supported models to skip this step. Then, adjust the settings. For your first print, use the default settings the slicer has for your resin. Don’t mess with exposure times first – if you’re using the resin I recommended, the default settings work 9 times out of 10. If your print is too thin later, you can bump exposure time by 1 or 2 seconds, but not on the first go. Save the file as an .stl or whatever format your printer uses, put it on a USB drive, and plug it into the printer.
Now, hit print. Take a deep breath. The first few layers are the most important – this is when the build plate is sticking to the print, so watch those first 10 layers. If the print looks like it’s pulling away from the build plate, hit pause or stop immediately. Don’t wait for the whole print to fail. I can’t tell you how many times a new user has texted me at midnight saying their print is ruined, and it’s because they didn’t watch the first 5 minutes. Most printers have a little camera now (the ones I sell do) so you can check on it from your phone if you’re in another room. That’s a game-changer for beginners.
Once the print is done, that’s when the fun (and slightly stinky part) starts – cleaning it. Don’t try to handle the print right away, it’s still wet with uncured resin. Remove the build plate from the printer, pop the print off gently (use a plastic spatula, not metal, you might scratch the build plate), then drop it into your tub of IPA. Make sure the print is fully submerged, then swish it around for like 5 minutes. You’ll see all the excess resin coming off into the IPA. Don’t scrub it yet, that can damage small details. After 5 minutes, take it out and use a lint-free cloth to gently wipe off any remaining resin. If there are tiny crevices, use a soft toothbrush to get in there.
Then, curing. This is the step that a lot of people skip, and their print stays sticky forever. You need a UV curing station, or even just a UV light – like the LED light strips people use for grow lights, or even sunlight if you live somewhere sunny. But don’t leave it in sunlight for too long, you can warp the print. Put the print in the curing station for like 5 minutes on each side, depending on the size. The print should feel hard and smooth when you’re done, not tacky. If it’s still sticky, it didn’t cure all the way, either because the exposure time was too short during printing, or you didn’t clean all the excess resin off.
Now, troubleshooting. Let’s be real, your first print will have issues. That’s normal. The most common problems: prints not sticking to the build plate. 9 times out of 10, that’s because the build plate wasn’t level, or it was dirty. Wipe the build plate with IPA every few prints, make sure it’s nice and clean. Another common issue: layers look jagged or not fully cured. That’s usually either exposure time is too short, or the FEP film is dirty. Wipe the FEP film with a soft cloth and a little IPA, don’t use paper towels. And if your print has little holes in it, that’s because there were bubbles in the resin when you poured it. Give the resin a quick stir before you pour, and let it sit for a minute to let bubbles rise to the top – you can skim them off with a toothpick if you want.
Wait, a quick safety note: resin fumes aren’t great. Don’t print in a closed room with no ventilation. Open a window, or put a small fan near the printer to circulate air. I always tell my customers to print in a garage or a well-ventilated room at first, especially if they’re new. You don’t want to be breathing in those fumes all day. Also, store resin in a cool, dark place – don’t leave it out in sunlight, that will cure it inside the bottle, which is useless.
Now, once you’ve got that first tiny print done, that feeling is awesome, right? You made something with your own hands that’s detailed enough to see every little line. If you’re thinking about scaling this up – maybe you want to make custom figures, or parts for small projects, or even sell prints – resin printers are way better than FDM for that, because the detail is insane. I’ve had designers who switched from FDM to our printers and went from selling 10 prints a month to 100, because people love how crisp the resin prints are.
Wait, if you’re reading this and you’re still on the fence about getting a resin printer, or you’ve already got one and you’re stuck, I’m here to help. I supply these printers personally, so you can reach out to me if you have questions about setup, settings, even what resin works best for your needs. No automated chat, no 24-hour wait – I’ll reply as soon as I can. Whether you’re a total newbie or you’ve been 3D printing for years and want to upgrade, I can help you find the right printer for your budget and goals.
Before I sign off, a quick recap for anyone who just skimmed: unbox slow, level that build plate, use the right resin, start with small short prints, clean and cure properly, and don’t panic if your first print sucks. It’s part of the process.
If you’re ready to take the plunge and start your resin 3D printing journey, feel free to reach out to discuss your needs, compare models, or get answers to any questions you have. I’m here to make this easy, not complicated.
Jewelry 3D Printer References:
- ASTM International. (2020). Standard Guide for Resin 3D Printing for Desktop Applications.
- 3D Printing Industry. (2022). Beginner’s Guide to Resin 3D Printer Setup and Maintenance.
- Smith, J. (2021). Troubleshooting Common Issues in Resin 3D Printing. Journal of Additive Manufacturing for Small Businesses, 12(3), 45-52.
- National Institute for Occupational Safety and Health (NIOSH). (2019). Safety Considerations for Desktop Resin 3D Printing.
Hangzhou Originator 3D Technology Co., Ltd.
Hangzhou Originator 3D Technology Co., Ltd. is one of the most experienced resin 3d printer manufacturers and suppliers in China. With abundant experience, we warmly welcome you to wholesale high quality resin 3d printer made in China here from our factory. Contact us for more details.
Address: Room 403, Building 2, Block B, Heda Incubation Park,No. 452, 6th Avenue, Xiasha, Qiantang District,Hangzhou, Zhejiang, China
E-mail: Sales@originator3d.com
WebSite: https://www.originator3d.com/
