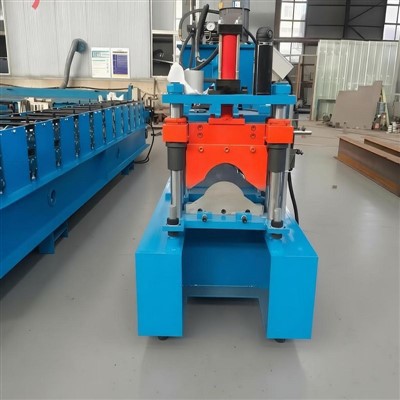
Roof Ridge Cap Roll Forming Machine If you’re running a metal fabricating shop, stamping plant, or any operation that relies on consistent, high-quality embossed metal parts, you know how fast wear and tear can derail your production. I’ve been a sales lead at a metal sheet embossing machine supplier for over 12 years, and I’ve seen dozens of clients struggle with premature failures on their machines’ key components—things like embossing rolls, die sets, feed rollers, and sheet guides. The number one complaint I hear? “We’re replacing rolls every 6 months and our machine downtime is killing our turnaround times.” The good news is that most of these issues boil down to choosing the right wear-resistant materials for those core parts. Today, I want to break down exactly what we use in our embossing machines, why they work, and how they solve real-world problems for our clients. Let’s start with the most critical part of any embossing machine: the embossing rolls. These are the two (or more) cylindrical tools that press into the metal sheet to create every pattern—from subtle decorative textures to heavy-duty grip patterns for construction or automotive parts. If the rolls wear down, your pattern will start to get fuzzy, uneven, or inconsistent, leading to scrap parts and unhappy clients. For the base of our embossing rolls, we start with high-strength alloy steel—specifically 4140 chrome-moly steel. It has a high tensile strength, which means it can handle the massive pressure needed to emboss thick steel, aluminum, or copper sheets without bending or deforming. But 4140 alone isn’t tough enough to resist the constant friction of metal sliding across its surface, especially when you’re running high-volume production. That’s where the wear-resistant coatings come in. For the roll surfaces, we use two primary treatments, depending on the client’s needs. For standard applications like embossing stainless steel sheets for appliance panels, we apply hard chrome plating. Wait, I know there’s some debate about chrome plating these days, but for our use case, it’s still one of the most cost-effective and durable options for mid-volume runs. The hard chrome layer we apply is 0.002 to 0.005 inches thick, with a surface hardness of 65 to 70 HRC (Rockwell C scale)—that’s twice as hard as tool steel, so it resists scratching and wear far better than uncoated rolls. But for clients running 24/7 production, like those making roofing materials or metal siding for construction, we switch to ceramic matrix composite (CMC) coatings. CMCs are made of hard ceramic particles (like aluminum oxide or titanium carbide) bonded with a metal matrix, so they combine extreme hardness with impact resistance. Their surface hardness is 80 to 85 HRC, and they can withstand temperatures up to 1,800°F, which is a huge plus if you’re working with pre-heated metal sheets for thicker gauges. I had a client in Texas last year who was running 16-gauge hot-rolled steel for shipping container panels, and they were replacing their standard chrome-plated rolls every 8 months. We swapped them for CMC-coated rolls, and they haven’t needed to change them in 26 months. That’s a 3x reduction in downtime, and they saved over $15,000 a year on replacement parts alone. Next up: die sets, which are the matching upper and lower tools that work in tandem with the embossing rolls for more complex, 3D embossing patterns. Die sets take even more punishment than rolls, because they’re often subjected to higher point loads and can get nicked if a small metal shard gets trapped between the die and the sheet. For our die sets, we use D2 tool steel as the base material. D2 is a high-carbon, high-chromium tool steel that’s known for its excellent wear resistance and toughness—way more than standard carbon steel. It has a hardness of around 60 HRC when heat-treated, which is perfect for resisting abrasion from metal sheets and debris. But even D2 can get pitted or develop surface cracks over time, especially if you’re working with sharp, abrasive materials like galvanized steel. So we add a secondary treatment here: nitriding. Nitriding is a process where we heat the die in a nitrogen-rich atmosphere at around 950°F, which diffuses nitrogen into the top 0.015 to 0.030 inches of the die surface. This creates an extremely hard, wear-resistant layer called a nitride case, with a surface hardness of 1100 to 1200 HV (Vickers scale)—that’s way harder than HRC, which is why HV is often used for very hard surfaces. Nitrided die sets don’t need re-coating as often as chrome-plated parts, and they resist corrosion too, which is a big win for outdoor applications where humidity or moisture is a factor. We had a client in the automotive parts industry who was making fuel tank brackets embossed with a textured pattern, and their old die sets were developing surface cracks every 10 months, leading to uneven patterns and scrap. Swapping to nitrided D2 die sets cut their die replacement time to every 3 years, and their scrap rate dropped from 7% to less than 1%. That’s a massive improvement for their bottom line. Another often-overlooked key component is the feed rollers. These are the rubber or metal rollers that grip the metal sheet and pull it through the embossing machine at a consistent speed. If feed rollers wear out, they start to slip, leading to misaligned patterns, uneven sheet feeding, and even jams that can damage the entire machine. For feed rollers, we use a combination of materials depending on the gauge of metal being processed. For thin sheets (20 gauge and thinner), we use urethane-coated steel rollers. Urethane has excellent grip, it’s resistant to abrasion, and it doesn’t scratch soft metals like aluminum or copper. We use a 90A durometer urethane coating, which is hard enough to resist wear from repeated contact with metal sheets but flexible enough to create a strong grip without leaving marks. For thicker sheets (16 gauge and up), where the gripping force is higher, we switch to cast iron feed rollers with a precision-ground surface. Cast iron is naturally more wear-resistant than steel, and its textured surface provides a better grip for thicker, heavier metal sheets. We machine the feed rollers to within 0.001 inches of tolerance, so they run smoothly without slipping, even at high production speeds. I once worked with a metal stamping shop that was using generic rubber feed rollers on 14-gauge steel, and they were replacing the rollers every 2 months because the rubber wore down and lost grip. Swapping to our cast iron feed rollers (we add a light coating of anti-slip lubricant for initial runs) meant they haven’t replaced them in 4 years. The last critical component I want to cover is the sheet guides. These are the stationary metal bars or plates that keep the metal sheet aligned as it moves through the embossing machine. If the guides are worn, the sheet can drift to one side, leading to off-center patterns, misalignment with the rolls, and even damaged parts. For sheet guides, we use PTFE (polytetrafluoroethylene) impregnated aluminum bronze. Aluminum bronze is a strong, wear-resistant alloy that’s far more durable than standard steel, and adding PTFE (the same material used in non-stick pans) gives it self-lubricating properties. That means the guides don’t need external lubrication, which eliminates mess and the risk of lubricant getting on the metal sheet (a big no-no for parts that need painting or coating). The PTFE reduces friction between the guide and the metal sheet, so there’s no excessive wear, even as thousands of sheets pass through the machine. We also machine the sheet guides to a smooth, flat finish, with edges rounded to prevent scratching the metal surface. A client in the appliance industry was having issues with scratched stainless steel sheets from their old steel sheet guides, which were also wearing unevenly. Swapping to our PTFE-impregnated aluminum bronze guides cut their scratch rate from 3% to less than 0.1%, and the guides have lasted 5 years with no replacement. Now, I want to be clear: there’s no one-size-fits-all solution here. The wear-resistant material you choose depends on several factors: the type of metal you’re embossing (thin vs. thick, soft vs. abrasive), your production volume (low, medium, or high), the required pattern detail, and your budget. For small businesses running low-volume prototypes, standard chrome-plated rolls and D2 tool steel dies might be more than enough, and they’re affordable. For large-scale production runs 24/7, investing in CMC rolls and nitrided die sets will save you far more money in downtime and replacement parts over time than the initial cost difference. I’ve seen too many clients try to cut corners by using cheaper, less wear-resistant materials, only to end up paying more in the long run from missed deadlines, scrap parts, and emergency maintenance. That’s why at our company, we work with every client to assess their specific needs, not just sell them the most expensive parts. For example, a client making custom metal signs (low volume, soft aluminum) might only need uncoated mild steel rolls and dies, while a client making structural metal decking (high volume, thick steel) needs the toughest materials we offer. If you’re experiencing frequent downtime, uneven embossed patterns, or high scrap rates, it’s worth taking a look at your machine’s key components and what they’re made of. Even small upgrades to wear-resistant materials can transform your production efficiency and save you thousands of dollars a year. If you’re in the market for a new embossing machine, or you’re looking to upgrade the components on your existing machine, feel free to reach out to our team to discuss your specific needs. We have decades of experience working with metal fabricators, construction companies, automotive parts manufacturers, and more, and we can help you find the right solution for your operation. Whether you need a custom embossing machine, component upgrades, or ongoing maintenance support, we’re here to help you keep your production running smoothly.
References Metal Sheet Embossing Machine

- ASM International. (2007). Tool Materials for Metal Forming. ASM Handbook, Volume 14: Forming and Forging, 10th ed.
- Budinski, K. G. (2010). Wear-resistant Materials: Properties and Selection. William Andrew Publishing.
- Dillon, E. W. (2019). Metal Embossing Technology and Equipment. Industrial Press Inc.
- Donachie, M. J., Jr. (2000). Steel: Microstructure and Properties. ASM International.
- Tuszynski, T. (2015). Coatings for Wear Resistance in Industrial Applications. Surface Engineering, Volume 31, Issue 10, 721-728.
Botou Shengda Cold Forming Machinery Equipment Manufacturing Co., Ltd.
Address: Liuxin Village, Botou Town, Botou City, Cangzhou City, Hebei Province
E-mail: cangzhoushengda888@163.com
WebSite: https://www.sdrfm.com/
